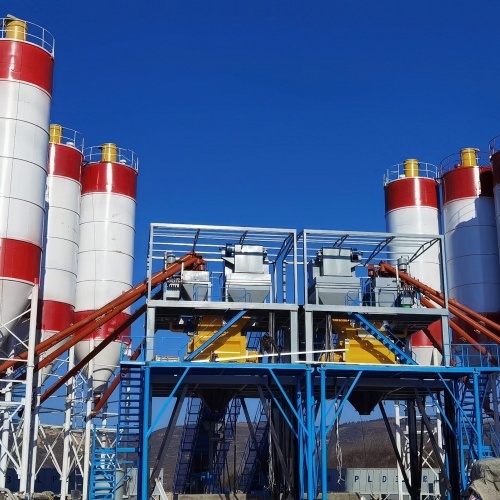
An HZS120 concrete mixing plant carries a theoretical rating of 120 m³/h. On a real job site, expect roughly 84–96 m³/h — about 70–80% of the nameplate figure. This article explains how that theoretical number is calculated, why actual output always falls short, the six factors that create the gap, and five strategies that narrow it. It is written for contractors and ready-mix operators comparing 混凝土配料站 before they request a quote.
HZS120 Concrete Mixing Plant: Key Capacity Numbers
- Theoretical capacity: 120 m³/h (60 batches of 2 m³ per hour at a 60-second cycle)
- Actual output: 84–96 m³/h in normal production — 70–80% of theoretical
- Best case: 90–100 m³/h in fully automatic, non-stop operation
- Cycle time: 60 s standard; 52 s with pre-feeding technology
- Biggest loss factor: transport vehicle turnaround — every 2-minute delay costs roughly 4 m³/h of output
HZS60 vs HZS120 vs HZS180: Capacity at a Glance
| 模型 | Theoretical Capacity | 实际产出 | Daily Output (8–10 h) | Best Fit |
|---|---|---|---|---|
| HZS60 混凝土搅拌站 | 60 m³/h | 40–50 m³/h | 400–500 m³ | Medium projects, ready-mix yards |
| HZS120 concrete mixing plant | 120 m³/h | 84–96 m³/h | 670–960 m³ | Medium-large projects |
| HZS180 混凝土搅拌站 | 180 立方米/小时 | 126–144 m³/h* | 1,000–1,400 m³* | Large projects, high-demand sites |
*HZS180 figures assume the same 70–80% efficiency factor measured on the HZS60 and HZS120. Before you size a plant, confirm the practical output for your mix designs and truck dispatch with the manufacturer.
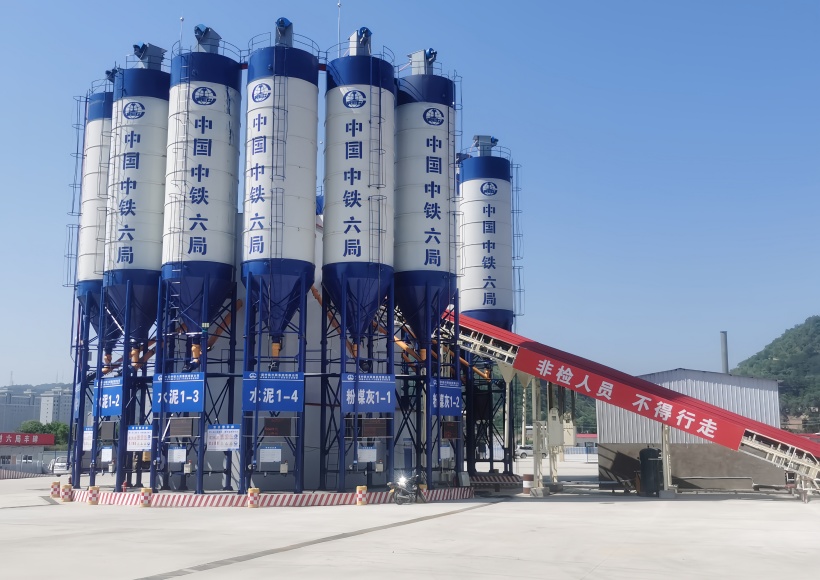
HZS120 Concrete Mixing Plant: Theoretical vs Actual Capacity
1.理论容量计算模型
The “120” in the HZS120 model name refers to its theoretical maximum output of 120 m³/h. Here is the calculation basis we use when checking a plant’s capacity:
- 单次卸料容量:2 立方米(JS2000 混合器标准配置)
- 理想工作周期:60 秒/周期
- 每小时循环次数:60 分钟 ÷ 1 分钟/周期 = 60 个周期
- 理论输出:60 个循环 × 2 立方米 = 120 立方米/小时
2.实际输出范围
In real production, output typically settles between 84 and 96 m³/h — 70% to 80% of the theoretical value. That gap is not a defect; it is the normal cost of transport intervals, manual operations and the occasional stoppage:
| 生产条件 | 实际输出范围 | 效率利用率 |
| 最佳运行条件(全自动/不间断) | 90-100 立方米/小时 | 92% |
| 正常生产(包括运输间隔时间) | 80-90 立方米/小时 | 80% |
| 有限条件(加载困难/失败) | 60-70 立方米/小时 | 55% |
Six Factors That Limit HZS120 Concrete Mixing Plant Output
1.运输调度协调
- 最佳实践:搅拌车周转时间不超过 2 分钟(生产能力超过 100 立方米/小时)
- 常见瓶颈:
- 运输车辆调度不及时(每延迟 2 分钟,产量就会减少 4 立方米)
- 不合理的装载区布局
2.原材料供应的稳定性
- 砂石含水量高导致运输拥堵
- 水泥仓中的结块对连续卸料的影响
- 螺旋输送机堵塞
3.混合循环优化
- 标准处理时间(共 60 秒):
- 进料和混合阶段:30 秒
- 卸载操作时间:15 秒
- 喂食准备时间:15 秒
- 技术升级:预喂料技术可将循环时间缩短至 52 秒
4.材料特性的影响
- 强度等级差异:C30 混凝土每批的搅拌时间比 C50 短 10-15 秒。.
- 骨料含水量过高:这会导致 20% 计量效率降低。.
• Specialty concrete production: Fiber-reinforced concrete requires a longer mixing time (resulting in an approximately 25% reduction in production).
5.设备维护
- 常见故障影响:
- 衬垫磨损(间隙 > 5 毫米时,10% 效率降低)
- 传感器故障(导致计量错误,影响自动化生产)
- 气缸密封失效(每批卸载延迟 3-5 秒)。.
6.环境和人为因素
- 气候影响:气温低于 -10°C 时,产量减少 30%(需要额外的骨料预热)。.
- 操作技能:新手操作员的效率比经验丰富的操作员低 15-20 m³/h。.
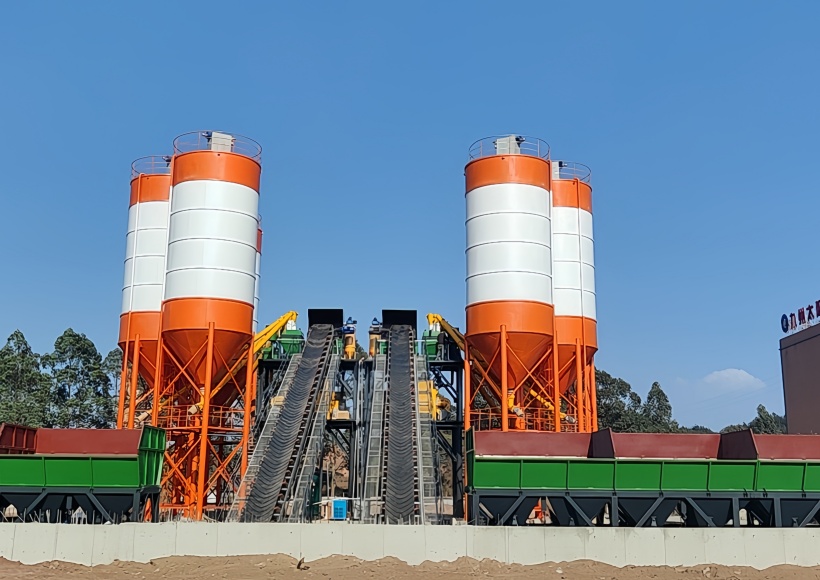
Five Practical Ways to Boost HZS120 Concrete Mixing Plant Capacity
1.设备升级
• Use larger transport vehicles (reduces turnover frequency)
• Install a real-time aggregate moisture content monitoring system
• Improve moisture-proofing facilities (to prevent cement compaction)
2.生产管理优化
- 车辆调度:保持两辆车随时可以装货(确保连续装货)
- 维护系统:每天清洁主机
- 人员培训:标准化操作可提高效率 8%
3.改进流程
- 采用预混合工艺,缩短混合时间
- 优化骨料分级,提高输送效率
- 采用先进的计量和控制系统
4.智能监控应用
- 安装传感器监测 设备 运行状态
- 实施实时生产数据收集系统
- 建立预警机制,提前发现故障
5.定期绩效评估
• Conduct monthly production capacity analysis
- 每季度进行设备性能测试
- 年度检修和升级规划
Common Problems and Fixes for the HZS120 Concrete Mixing Plant
1.实际产出与理论产出存在差异的原因
理论产量是在零等待时间、全自动化和理想混合比条件下计算得出的极限值。实际产量不可避免地会受到运输间隔、人工操作和故障排除等因素的影响。.
2.设备选择指南
- HZS120 混凝土搅拌站适用场景:日产量小于 800 立方米的中型项目
• HZS180 混凝土搅拌站 Applicable Scenario: Large-scale projects with daily production demand greater than 1000 m³
3.生产评估标准
- 合格指标:持续保持 80 立方米/小时或以上的生产率(包括正常损耗)
- 异常故障排除流程:
① 检查循环时间是否超过 60 秒
确认运输车辆的等候时间少于 5 分钟 ② 确认运输车辆的等候时间少于 5 分钟
检查总供应量的连续性
验证计量系统的准确性
HZS120 Concrete Mixing Plant FAQ
What is the actual capacity of an HZS120 concrete mixing plant?
In normal production, an HZS120 concrete mixing plant delivers about 84–96 m³/h, roughly 70–80% of its 120 m³/h theoretical rating. Under optimal conditions it can reach 90–100 m³/h.
Why does actual output fall below theoretical capacity?
Theoretical capacity assumes zero waiting time, full automation and ideal mix ratios. In practice, transport vehicle turnaround, material supply interruptions, operator skill, maintenance condition and weather all reduce output.
How can I increase the output of an HZS120 concrete mixing plant?
Shorten the mixing cycle with pre-feeding technology (from 60 to 52 seconds), keep two trucks waiting at the loading point, monitor aggregate moisture, schedule preventive maintenance, and run monthly production capacity analyses.
HZS120 Concrete Mixing Plant: Final Verdict
The realistic working range for an HZS120 concrete mixing plant in good condition is 80–100 m³/h. Equipment configuration, production management, maintenance and intelligent monitoring each pull output in a different direction; improve all four and the gap between rated and actual capacity narrows noticeably. Set up a monthly capacity check and a quarterly production review, and treat every drop below 80 m³/h as a fault to investigate, not a number to accept.
One last note from our workshop: never size a plant from the nameplate alone. The HZS120 is a strong fit for medium-sized projects with daily demand under 800 m³, but the same machine under-delivers on a site with poor truck flow. 砼信机械 offers free on-site surveys and production plan design; our engineers help you match the 配置 to the job so you get the output you are paying for. Contact our technical team for a personalized solution.