
An HZS50 station is sold as a 50 cubic meter per hour plant. Owners who buy on that figure often find the shift ticket total does not match it. The gap is not a machine fault. It comes from cycle time, truck flow and how the plant is run on a real site. Any honest discussion of HZS50 concrete batching plant capacity has to start there.
This guide works through that question with numbers from working sites in three countries. It covers the cycle math, four places where output slips, the benchmarks worth comparing against, and the adjustments that lift a plant without replacing it. Nothing below depends on a single brand or a single brochure figure.
What the 50 m3/h Rating Actually Covers
Nominal, Technical and Working Capacity
Three figures need to stay apart during planning. Nominal capacity is the brochure number. Technical capacity is what the plant reaches with clean material and a free loading bay. Working capacity is what a site dispatches across a full shift, and every serious project is built on that third figure rather than on the first.
The Assumed Batch and Cycle
The published HZS50 concrete batching plant capacity assumes a one cubic meter batch and about 72 seconds between discharges. Change either input and the ceiling moves at once. Dry mixes, low slump and small aggregate loads push cycle time up, and one extra second per cycle costs roughly 0.7 cubic meters of hourly output.
Why Suppliers Publish the Ceiling
Suppliers publish the ceiling because it is the only figure every buyer can compare on equal terms. It assumes material always ready and a truck always waiting at the bay. It is a design limit rather than an average, and no site runs at a limit for eight hours straight without a pause for cleaning or a shift change.
The Cycle Math Behind HZS50 Capacity
Batch Size and Drum Rating
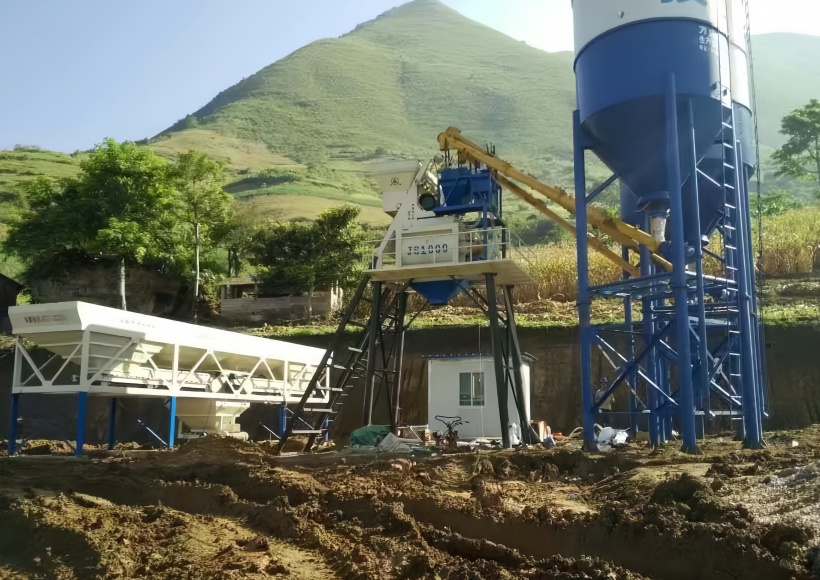
The JS1000 mixer behind most HZS50 plants takes one cubic meter of compacted concrete per batch. Rated output assumes the drum fills to that line on every cycle. Filling above it shortens mixer life, and filling below it cuts output in direct proportion to the shortfall across the whole shift.
Operators sometimes load 0.85 cubic meters to protect the machine on hard aggregate. That choice costs about 7.5 cubic meters per hour at full cycle speed, or sixty cubic meters across a normal day. It is a fair trade on wear parts, as long as the loss is planned rather than discovered at month end.
Mixing Time Per Cycle
Dry mixing, wet mixing and discharge together set the floor on cycle time. A well kept JS1000 runs 60 to 70 seconds in the drum on standard mixes. Worn blades, a slack drive belt or low hydraulic pressure add seconds, and those seconds show up as missing cubic meters on the shift sheet.
Blade clearance is the usual suspect behind a slow cycle. When the gap between blade and liner passes 10 mm, mixing efficiency drops and operators extend the cycle to reach the specified slump. A liner and blade check every 500 hours keeps the cycle inside its design window without surprise stops.
Weighing and Discharge Overlap
Modern control systems weigh the next batch while the current one mixes. When an operator runs the plant by hand, that overlap disappears and cycle time stretches by 15 to 25 seconds. The same machine then delivers about 40 cubic meters per hour instead of the rated fifty on a full shift.
Automatic batching is the cheapest upgrade on an HZS50. The hardware is usually already fitted, and the gain comes from using the recipe memory and the automatic cycle instead of hand control. Most crews adapt within two shifts, and the gain stays in place for the life of the plant.
Four Places HZS50 Concrete Batching Plant Capacity Slips
Truck Interchange and Site Traffic
A mixer truck takes three to four minutes to spot, load and leave the bay. With eight trucks in a queue and one loading point, the plant waits longer than it mixes. Site layout matters as much as the machine, and a wider exit lane can return five cubic meters per hour on its own.
Loading bay design follows the same logic as the drum. Trucks that must reverse into position lose forty seconds each, which repeats fifty times an hour. A drive through bay with a twelve meter approach removes that step, and the cost is a few meters of hardstanding rather than a new plant.
Aggregate Feeding and Stockpile Condition
The loader fills the aggregate bins between batches. Wet sand that bridges in a hopper, or a stockpile pushed too far from the bins, adds a minute to every cycle. Keeping three days of graded material under cover removes most of this loss on most sites without any equipment change.
Bin volume matters on short cycles. Bins sized for fifteen batches let the loader work in blocks instead of sprinting between pours. Sizing the stockpile bay for two grades and one blending sand covers most HZS50 work without frequent changeovers in the middle of a pour.
Cement Supply and Silo Pressure
A cement silo that runs low slows the screw conveyor and lengthens the weigh hopper cycle. Two silos on a changeover valve keep supply steady while one is being refilled from a tanker. Blocked dust collectors do the same damage, since pressure builds and feeding turns uneven between batches.
Humidity is the silent loss here. Cement that picks up moisture in a silo aerates badly, and the screw runs at reduced rate for days before anyone notices the drop. Silo aeration on a timer and a filter clean every two weeks protect the feed rate through the wet season.
Operator Rhythm and Shift Change
Shift change, meal breaks and paperwork all stop the drum for minutes at a time. Plants that keep a spare operator on the floor and hand over records at the control desk lose twenty to thirty minutes less per shift than plants that stop for a handover meeting in the site office.
Crew size also shapes the rhythm. A five person crew covers batching, loader work, dispatch and quality checks with one spare hand for the unexpected. A four person crew has no spare, so every delay lands on the plant instead of on a person who can absorb it.
Benchmarks for HZS50 Concrete Batching Plant Capacity
What the Field Records Show
Field records from HZS50 plants in three countries give a realistic spread of working figures. The table groups them by how the plant is run rather than by machine age, because management explains more of the variation than equipment ever does on the same model.
| Operating condition | Hourly output | Ten hour shift | What it looks like |
| Well run, single bay, six trucks | 42 to 45 m3 | 420 to 450 m3 | New plant, covered stockpile, automatic cycle |
| Normal commercial operation | 32 to 36 m3 | 320 to 360 m3 | Mixed fleet, some waiting at the gate |
| Congested site, manual control | 22 to 26 m3 | 220 to 260 m3 | Queue outside the gate, hand batching |
| Wet material, frequent stops | 18 to 22 m3 | 180 to 220 m3 | Bridging aggregate, blocked filters |
The second row is the number to plan a project on. A 34 cubic meter hour average across a ten hour day moves 340 cubic meters, enough for a mid rise floor slab with columns and a service core in one pour cycle without a second plant on standby.
Reading the Table Against Your Project
Match your own site to the row that looks like it. A plant on a city site with tight gates behaves like the congested row even when the machine is new and clean. A rural plant with covered stock and a long pour window reaches the first row after a season of steady discipline.
Seasonal Movement
The HZS50 concrete batching plant capacity figure moves with the season as well. Summer pours with hot cement run shorter cycles, and winter work with cold aggregate runs longer ones. Planning output by season beats planning by brochure figure, especially on sites that pour all year round for the same customer base.
How to Measure HZS50 Concrete Batching Plant Capacity on Your Site
Benchmarks from other sites only help once your own HZS50 concrete batching plant capacity numbers exist on paper. A week of simple records turns a vague complaint about slow output into a list of specific losses, each with a fix and a price attached to it before any money is spent.
What to Log Every Hour
Record batch count, truck count, cubic meters dispatched, start and stop times, and the reason for every stop longer than two minutes. A paper sheet at the control desk works as well as software, provided the operator fills it in during the shift rather than at the end of the week.
Add one column for material condition. Sand moisture, aggregate grading and cement silo level explain most slow cycles, and those values are easy to record at the change of a shift with a moisture meter and a quick visual check of the stockpile face. Two minutes at each shift change is enough to catch a change in the sand pit before it reaches the batching tower.
Read the Log After Seven Days
After a week the pattern is clear enough to act on. Divide dispatched cubic meters by running hours to get working capacity, then group the stop reasons by cause. Idle time caused by trucks, material or maintenance each points to a different fix with a different cost.
Comparing Against Benchmarks
Set the measured HZS50 concrete batching plant capacity against the table above. A gap of ten cubic meters per hour against the normal row is worth a full review of layout and dispatch. A gap of three is usually dispatch timing, and the log will show it in the stop column.
Raising HZS50 Concrete Batching Plant Capacity Without Replacing the Plant
Mixing Cycle Work
New blades and a checked gearbox often return five seconds per cycle on a worn machine. That is about 3.5 cubic meters per hour, or 28 cubic meters across an eight hour shift. The parts cost less than a week of that extra volume at any normal concrete price in any market.
Discharge door timing is the other easy gain on the same visit. A worn cylinder that takes two seconds longer to open repeats fifty times an hour. Replacing the seal kit and re setting the door stop keeps the cycle inside the 72 second design window without touching the mixer drive.
Feeding and Discharge Work
Wider aggregate gates, a cleaned discharge chute and a second loading point shorten the non mixing part of the cycle. Most of these jobs cost less than a week of lost output and fit inside a scheduled weekend stop with a small crew and a welder on site.
Belt speed is worth a look on plants with a long incline between bins and tower. A conveyor running below design speed adds eight to twelve seconds to each batch, and a pulley change or a motor rewind restores the designed feed time for a modest parts bill.
Dispatch Discipline
Appointment loading, one dispatcher in radio contact with drivers, and a printed pour sequence keep trucks arriving when the plant is free. Sites that adopt this routine report ten to fifteen percent more dispatched volume with no equipment change and no extra capital at all.
The same discipline protects quality as well as speed. Concrete that waits in the drum past its workability window gets dumped or reworked, and both outcomes consume capacity that was already paid for. Quality losses hide inside the same hourly figure as speed losses do.

What HZS50 Concrete Batching Plant Capacity Costs per Cubic Meter
Energy per Cubic Meter
The HZS50 plant draws roughly 90 to 100 kW with the mixer, conveyors, screws and dust collectors running together. At a 0.75 load factor and 0.1 USD per kWh, energy adds about 0.8 USD to each cubic meter, small beside cement and aggregate, worth tracking all the same.
Labour per Cubic Meter
Labour is the larger variable on most sites. A five person crew on a 340 cubic meter day carries about 1.3 USD per cubic meter when a shift costs 200 USD in wages. Output per crew hour, not mixer speed, sets that number, which is why dispatch gains beat motor upgrades.
Maintenance Reserve
Maintenance belongs in the same table as energy and labour. Blades, liners, belts and filters on an HZS50 cost about 0.4 USD per cubic meter over a year at normal output. A plant run hard with no liner change spends that money twice, once on parts and once on lost cycles.
How Layout Changes Working Capacity
Loading Bay and Truck Flow
A layout review costs nothing and often finds three to five cubic meters per hour in a single afternoon. The usual faults are a loading bay that forces reversing, a stockpile beyond the loader reach, and a weighbridge placed where trucks block the exit lane at peak.
Stockpile and Bin Placement
Aggregate bins on the mixer side of the tower shorten the loader cycle by half a minute. Cement silos placed for a straight screw run avoid the elbow that steals feed rate. Water and admixture tanks within reach of the operator cut the walk time between manual additions on every batch.
Washout and Waste Points
Washing and waste points matter on sites with strict discharge rules. A washout bay near the exit keeps returning trucks out of the loading queue, and that single decision protects the rhythm of the whole shift for the cost of one concrete slab and a settlement pit.
How Material Quality Moves Output
Sand Moisture
Wet sand is the most common capacity thief on an HZS50 in the rainy season. Each percent of moisture above the design value lengthens the feed cycle and forces a water adjustment that operators make by eye. A covered stockpile and a moisture reading at each shift remove the guesswork.
Aggregate Grading
Gap graded blends and oversized stone both slow the mixer on every cycle. Grading that matches the mix design keeps the cycle steady, and a washed supply usually pays for itself through shorter cycles and fewer rejected loads on the same pour at the same plant.
Cement Flow Behaviour
Fresh cement aerates well and feeds evenly through the screw. Cement held in a warm silo for weeks can compact, and the screw then delivers less per turn until the silo is emptied. Rotation of stock by delivery date is a simple habit that protects the weigh cycle at no extra cost.

When a Bigger Model Makes More Sense
Where the Break Point Sits
If measured HZS50 concrete batching plant capacity stays below 25 cubic meters per hour after the adjustments above, and demand is steady through the year, a larger plant pays back faster than a second HZS50. Twin plants double the crew, the site area and the maintenance load.
What an HZS75 Delivers
An HZS75 plant with a JS1500 mixer delivers about 70 cubic meters per hour at the same discipline level as the smaller station. The step suits projects above 400 cubic meters a day, while smaller pours still fit a single HZS50 across two shifts. Site access has to widen for the longer truck queue the bigger plant pulls in.
Two Shifts Before a Second Plant
A second shift usually costs less than a second plant on the same site. The drum, loader, silos and crew already exist, and the added cost is wages plus wear on parts. Sites that run two shifts on one HZS50 often cover 600 cubic meters a day without new capital.
What the HZS50 Concrete Batching Plant Capacity Means for Project Planning
Daily Volume Sets the Fleet
Pour planning starts from the daily volume, not the HZS50 concrete batching plant capacity figure printed on the brochure. A 340 cubic meter day needs eight to ten trucks on a 45 minute round trip, one loader, and a stockpile that covers the whole pour without a changeover in the middle of the morning.
Peak Pours
Peak pours break the average and deserve their own plan. A foundation mat that needs 150 cubic meters in four hours has to run at 38 cubic meters per hour, which means a clean stockpile, two loading bays and a spare operator on the floor for that morning only.
Sequencing Two Sites
Sequence the pours so the plant does not idle between them during the day. Two sites booked on the same day, one in the morning and one after lunch, keep the drum turning and spread the fixed cost of the crew across more cubic meters of paid output.
Maintenance Rhythm That Protects Output
Blade and Liner Checks
Output falls before breakdowns show on the ticket, and HZS50 concrete batching plant capacity falls with it. A liner check every 500 hours, a blade gap adjustment at the same interval, and a filter clean every two weeks keep the cycle inside its window without unscheduled stops on a pour day when trucks are already queued.
Filter and Screw Care
Dust filters and screw conveyors carry the material side of HZS50 concrete batching plant capacity. A blocked filter raises silo pressure, and a worn screw flight delivers less cement per turn. Both losses show first as longer weigh cycles rather than as an obvious failure.
Planned Stops Beat Failures
Record the blade gap and the cycle time together in the same log book. When the two drift apart, the plant is asking for maintenance before it fails. A planned stop on a Sunday costs a fraction of a mid pour failure on a Friday afternoon in front of a waiting customer.
Questions Buyers Ask About HZS50 Output
What is the real capacity of an HZS50 plant?
Between 30 and 36 cubic meters per hour in normal commercial operation, and 42 to 45 on a well managed site with covered material and automatic batching. The figure holds across brands, since the cycle math stays the same on every machine built to this size.
Why does my plant only reach 25 cubic meters per hour?
Truck waiting, hand batching and wet aggregate are the three common causes on most sites. A one week log separates them, and each has a different fix with a different price. Most plants recover five to eight cubic meters per hour once the main cause is removed.
Can an HZS50 reach 50 cubic meters per hour?
Only in short peaks with a full batch, dry material and a free loading bay at the same time. Planning a project on that figure leaves the schedule short by about a third, and the shortfall usually appears later as night pours and paid overtime.
Does aggregate size change capacity?
Yes, and the effect shows up on every cycle through the day. Larger coarse aggregate mixes faster, while wet fines slow the feed and lengthen the cycle. Grading control is part of capacity control, and a washed sand supply often pays for itself in cycle time alone across a season.
How many trucks does an HZS50 need?
Six to eight trucks of 8 to 10 cubic meters on a 45 minute round trip keep a 34 cubic meter hour plant supplied without a queue at the gate. Longer trips need proportionally more trucks, or a shorter pour window with a tighter dispatch plan.
Is a second shift cheaper than a bigger plant?
Below 400 cubic meters a day, yes in most markets. The second shift uses the plant already paid for, and the extra cost is wages rather than capital. Above that level, a larger plant usually wins on cost per cubic meter over a full year of steady demand.
What to Specify When Ordering
Contract Wording
Ask for guaranteed continuous output, not a peak rating on the data sheet. A supplier who will write 30 cubic meters per hour into the contract at a stated material condition is giving you the only HZS50 concrete batching plant capacity promise worth trusting, since it is tied to real work rather than a brochure page.
Core Components
Specify the mixer, the batching accuracy, the control system and the dust collection in the purchase order. Those four items decide whether the plant reaches its promised HZS50 concrete batching plant capacity in the first month or only in the first year after commissioning, and no discount on the order compensates for a weak control system.
Next Reading
For layout planning, the construction plan guide covers site preparation and bay placement. For budget work, the price analysis model sets the cost lines that capacity decisions affect, including power, crew and silo capacity. Both guides are written for the same plant size and the same working assumptions used in this article.
Tongxin Machinery builds HZS50 stations with the JS1000 mixer, automatic batching control and dust collection sized for continuous work. Send your pour schedule and site plan, and the engineering team will confirm the HZS50 concrete batching plant capacity your project can expect on each shift before you sign.