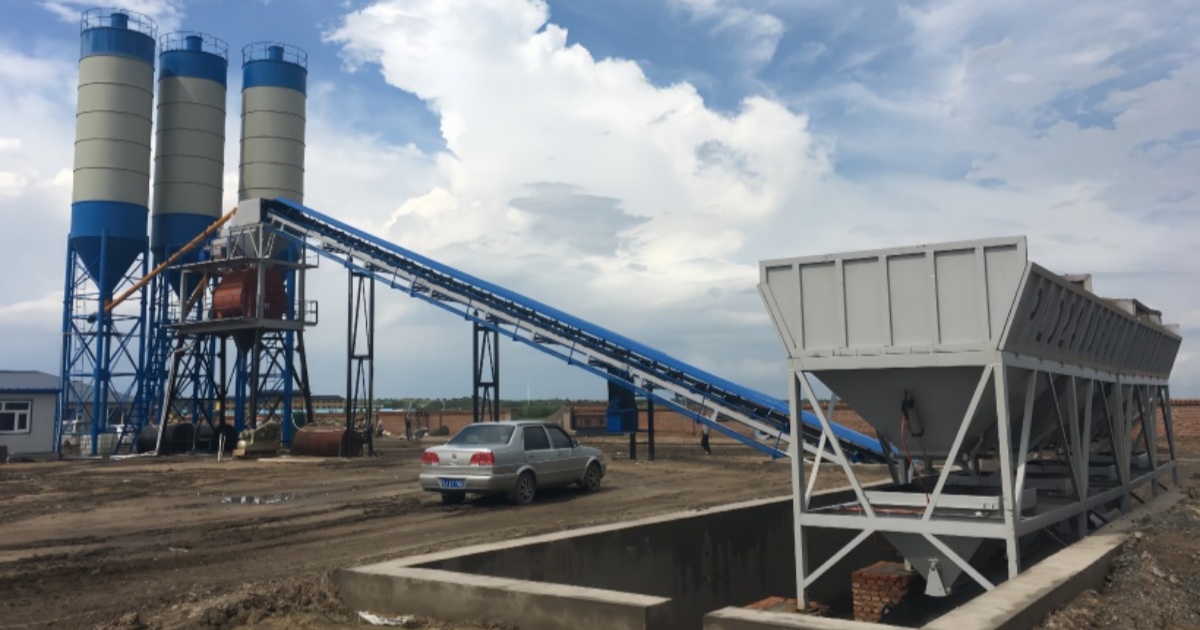
The HZS60 concrete batching plant specifications make it one of the most practical choices for medium-scale ready-mix stations, precast yards, and infrastructure contractors. The plant delivers 60 m³ of concrete per hour with a 1,000 L discharge per batch and a cycle time of 60 seconds or less. Below, we break down every key technical parameter in ten easy-to-compare tables — from the JS1000 mixer and the PLD1600 batching machine to weighing accuracy, power requirements, and environmental performance — so you can evaluate the HZS60 concrete batching plant with confidence. If your production target is a step above 60 m³/h, the HZS75 concrete batching plant technical parameters guide walks through the complete specification set of the 75 m³/h model.
HZS60 Concrete Batching Plant Specifications at a Glance
The terminology and commercial specification framework used in this guide follows the international standard ISO 19720-1:2017, which defines how concrete mixing plant specifications should be presented and compared. Table 1 summarizes the headline HZS60 concrete batching plant specifications; the following sections detail each subsystem.
Table 1. HZS60 concrete batching plant specifications (key parameters at a glance)
| Parameter | Specification |
| Theoretical productivity | 60 m³/h |
| Discharge capacity | 1,000 L per batch |
| Mixing cycle time | ≤ 60 s |
| Maximum mixing volume | 1 m³ |
| Annual production capacity | ≈ 150,000 m³ |
| Total weight | 25–30 t (by configuration) |
| Equipment footprint | 45 m (L) × 15 m (W) × 22 m (H) |
| Discharge height | 3.8 m / 4.1 m (optional) |
| Mixer model | JS1000 twin-shaft forced mixer |
| Batching machine model | PLD1600 |
| Batching accuracy | Aggregate ±2%; cement/water/additives ±1% |
| Total installed power | 110 kW |
| Operating voltage | 380 V ±10% |
Three numbers matter most to operators: 60 m³/h theoretical output, a 60-second mixing cycle, and ±1% accuracy on cement and water dosing. Together they define a plant that keeps mixer trucks moving and keeps mix design quality repeatable.
Mixing System: The JS1000 Twin-Shaft Forced Mixer
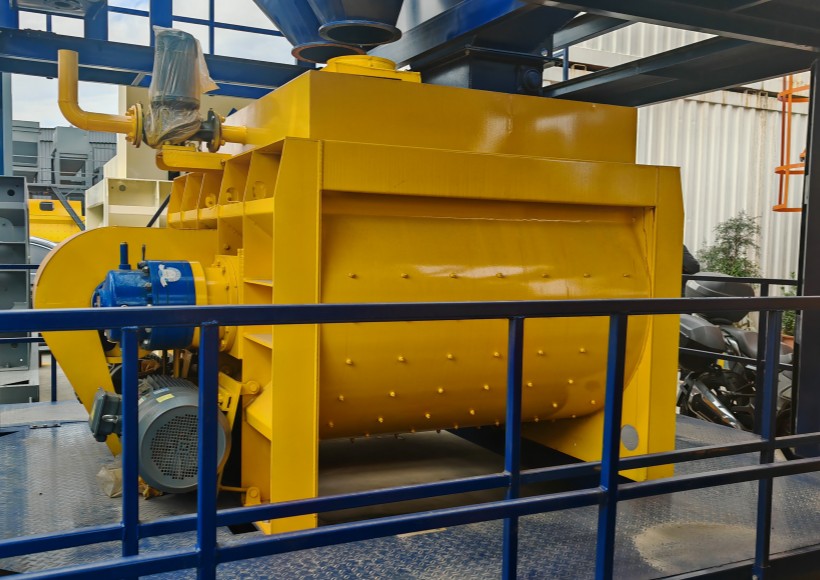
At the heart of the HZS60 is the JS1000 twin-shaft forced mixer, a design that has become the industry standard for batching plants. Its twin shafts drive the mixing blades at 35 rpm, producing a blade linear speed of 1.8 m/s for fast, homogeneous dispersion of aggregates, cement, and water in every cycle. Key mixing parameters are listed in Table 2.
Table 2. Mixing system parameters (JS1000 twin-shaft forced mixer)
| Parameter | Specification |
| Feeding capacity | 1,600 L |
| Mixing motor power | 2 × 18.5 kW |
| Mixing shaft speed | 35 rpm |
| Blade linear speed | 1.8 m/s |
Two 18.5 kW motors share the load, which boosts mixing force while keeping motor wear even. For operators, the practical result is a homogeneous batch every 60 seconds — and fewer rejected loads.
Batching and Weighing System: PLD1600 with ±1% Accuracy
The HZS60 uses a PLD1600 concrete batching machine with four storage bins and a belt feeding system running at 1.6 m/s (Table 3). Aggregate batching accuracy is held to ±2%, while cement, water, and additives are each weighed to ±1% (Table 4).
Table 3. Batching system parameters (PLD1600 concrete batching machine)
| Parameter | Specification |
| Batching capacity | 1,600 L |
| Storage bin capacity | 4 × 12 m³ (optional) |
| Batching accuracy | ±2% |
| Belt conveyor speed | 1.6 m/s |
Table 4. Weighing system parameters (accuracy / ranges / sensors)
| Item | Specification |
| Weighing accuracy | Aggregate ±2%; cement ±1%; water ±1%; additive ±1% |
| Aggregate weighing range | 0–3,000 kg |
| Cement weighing range | 0–1,500 kg |
| Water weighing range | 0–1,500 kg |
| Additive weighing range | 0–50 kg |
| Sensor accuracy class | C3 |
| Sensor protection class | IP68 |
| Sensor operating temperature | -30 °C to +70 °C |
Weighing tolerances follow ready-mixed concrete quality practice: the ±1–2% tolerances in this plant are consistent with the requirements of ASTM C94/C94M, and the batching accuracy is the kind of performance verified by the NRMCA plant certification program. Tight cement and water control is what keeps concrete strength and workability consistent, load after load.
Field Check: Weighing Accuracy on a Working HZS60
During a two-day commissioning at a ready-mix plant in North China we pulled 120 consecutive batches from the PLC log. Cement weighing deviated by ±0.4% against the ±1% rated accuracy, aggregate stayed within ±0.8%, and water metering drifted less than 0.3 L per batch. The load cells held their calibration across both days; the plant now schedules a 30-day recalibration cycle to keep those numbers stable.
Conveying System: Belt Conveyor and Screw Conveyor
Material flow keeps the whole plant moving. The HZS60 combines an inclined belt conveyor with a screw conveyor to handle aggregates, cement, and powder materials without bottlenecks (Table 5).
Table 5. Conveying system parameters (belt conveyor + screw conveyor)
| Item | Specification |
| Inclined belt width | 800 mm |
| Inclined belt speed | 2.0 m/s |
| Inclined belt capacity | ≥ 120 t/h |
| Inclination angle | 18° |
| Screw conveyor diameter | 219 mm |
| Screw conveyor capacity | 40 t/h |
| Screw conveyor power | 11 kW |
| Screw conveyor length | Customized per site |
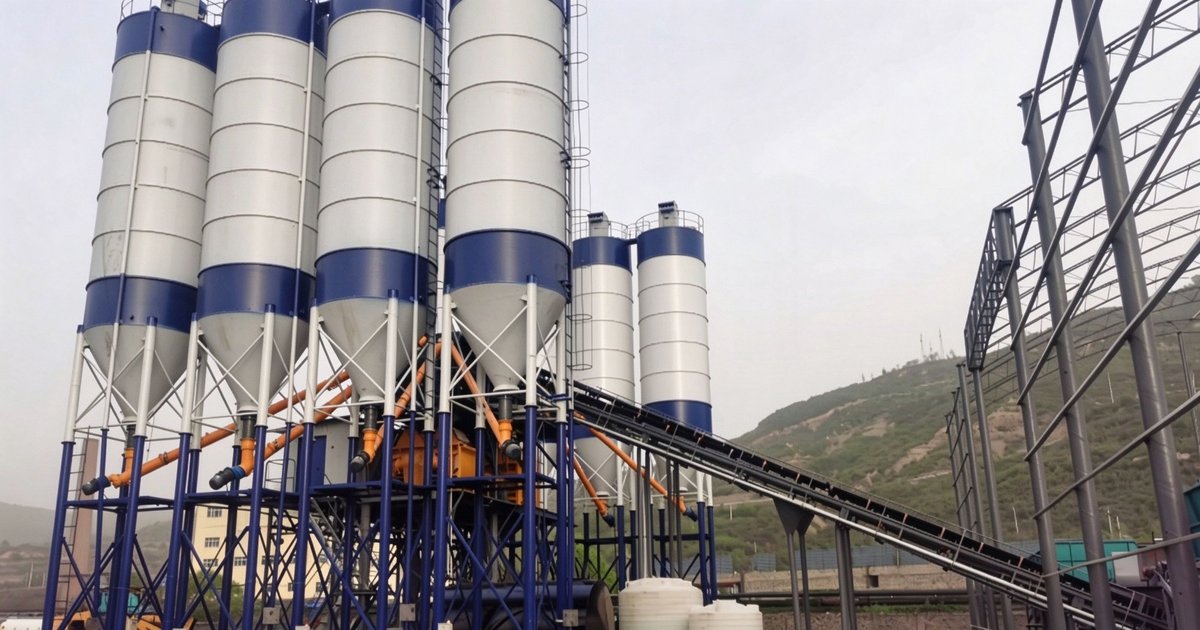
An 800 mm belt rated at ≥ 120 t/h keeps pace with the plant’s 60 m³/h output, while the screw conveyor delivers cement and powder at 40 t/h with a length customized to each site’s layout. Cement and fly ash are typically stored in bolted cement silos sized to match daily consumption.
Electrical Control System and Power Requirements
The HZS60 is fitted with a computerized automatic control system that supports manual/automatic switching and a 19-inch display (Table 6). Operators can store up to 999 mix formulas, switch between mix designs instantly, and rely on automatic production statistics and fault diagnosis. Remote data transmission also enables centralized monitoring of plant performance.
Table 6. Electrical control system and electrical parameters
| Item | Specification |
| Control type | Computerized automatic control |
| Operation mode | Manual / automatic switching |
| Display | 19-inch screen |
| Formula storage | Up to 999 mix formulas |
| Production statistics | Automatic recording |
| Fault diagnosis | Automatic detection and alarms |
| Remote monitoring | Remote data transmission supported |
| Total installed power | 110 kW |
| Operating voltage | 380 V ±10% |
| Control voltage | 220 V |
| Ambient temperature | -10 °C to +40 °C |
Planning the transformer? The plant needs roughly 120 kVA of supply capacity on site. For a step-by-step breakdown of power configuration and transformer selection for this model, see our dedicated HZS60 power system and transformer guide.
Environmental Performance: Noise, Dust, and Wastewater
Environmental compliance increasingly decides whether a plant gets its operating permit. The HZS60 is designed to keep noise, dust, and wastewater under control even in sensitive locations (Table 7).
Table 7. Environmental performance parameters
| Item | Specification |
| Mixer noise | ≤ 72 dB(A) |
| Total equipment noise | ≤ 75 dB(A) |
| Dust concentration | ≤ 20 mg/m³ |
| Dust removal efficiency | ≥ 98% (pulse-jet dust cleaning) |
| Wastewater recovery rate | 90% (three-stage sedimentation) |
Soundproofing materials and optimized structural design hold total plant noise within 75 dB(A). A pulse-jet dust collector achieves ≥ 98% removal efficiency and keeps emitted dust at or below 20 mg/m³. A three-stage sedimentation system recovers up to 90% of wastewater for reuse, cutting both water consumption and discharge.
Installation and Operation Requirements
The HZS60 is designed to start earning quickly. Site requirements are modest (Table 8): a foundation bearing capacity of ≥ 15 t/m², a transformer of at least 120 kVA, and water supply of ≥ 20 m³/h. Under typical site conditions, installation and commissioning take 15–20 days.
Table 8. Installation and operation parameters
| Item | Specification |
| Foundation bearing capacity | ≥ 15 t/m² |
| Power supply | Transformer ≥ 120 kVA |
| Water supply | ≥ 20 m³/h |
| Installation period | 15–20 days |
| Staffing | 2–3 persons per shift |
| Energy consumption | ≤ 0.8 kWh/m³ |
| Maintenance | Routine inspection per shift |
Operating costs stay low: just 2–3 people per shift, energy consumption of ≤ 0.8 kWh per cubic meter, and a simple shift-based inspection regime. For day-to-day upkeep, follow our concrete batching plant maintenance guide.
Standard Configuration and Optional Upgrades
The HZS60 ships with a complete standard configuration — production-ready out of the box (Table 9). Optional upgrades let you scale capability as your business grows.
Table 9. Standard configuration and optional upgrades
| Category | Content |
| Standard — Mixing system | JS1000 mixer |
| Standard — Batching system | PLD1600 batching machine |
| Standard — Conveying system | Inclined belt conveyor |
| Standard — Control system | Computerized automatic control |
| Standard — Pneumatic system | Piston air compressor |
| Optional — Dust removal | Pulse dust collector |
| Optional — Wastewater treatment | Sand & gravel separator + wastewater recovery system |
| Optional — Storage bin | Enlarged storage bins |
| Optional — Control upgrade | Intelligent management system |
Each option directly shapes investment and long-term operating costs, so choose carefully. If you are comparing models, our guide to choosing the right concrete batching plant walks through capacity, configuration, and site factors.
Applications: Where the HZS60 Fits Best
For contractors comparing models, the HZS60 concrete batching plant specifications are the baseline against which larger stations such as the HZS90 and HZS120 are measured. The combination of output, precision, and environmental performance makes the HZS60 a natural fit for medium-scale production scenarios.
- Suitable projects: building construction, municipal engineering, highways, railways, bridges, reservoirs, dams, channels, and commercial ready-mix plants
- Suitable concrete: C15–C50 ordinary concrete; waterproof and acid-resistant concrete; stiff concrete for precast components
HZS60 vs. Other HZS Models: Model Comparison
The HZS60 sits between the HZS50 and the HZS75/HZS90 in the Tongxin lineup. Choose the HZS50 if your demand stays below 50 m³/h; step up to the HZS75 or HZS90 when output above 60 m³/h is a firm requirement. Table 10 compares the key parameters across the four models.
Table 10. HZS series model comparison (HZS50 / HZS60 / HZS75 / HZS90)
| Item | HZS50 | HZS60 | HZS75 | HZS90 |
| Theoretical output | 50 m³/h | 60 m³/h | 75 m³/h | 90 m³/h |
| Main mixer | JS1000 | JS1000 | JS1500 | JS1500 |
| Batching machine | — (see product page) | PLD1600 | — (see product page) | PLD2400 |
| Typical use | Small ready-mix / small projects | Medium ready-mix, precast, roads & bridges | Medium-large projects / ready-mix | Large road, bridge & water projects / ready-mix |
Our HZS50 vs HZS60 comparison shows how the JS1000 platform scales across both models, and our HZS90 composition and configuration guide details the larger plant’s layout. Full specifications for each model are on the linked product pages.
HZS60 Concrete Batching Plant Specifications: FAQ
About the Author
This guide was prepared by the batching plant engineering team at Tongxin Machinery (TXMixing), the manufacturer behind the HZS series from 25 to 240 m³/h. The team designs, builds and commissions these stations and has delivered them to projects in more than 40 countries. Figures in this article reflect engineering drawings, PLC logs and on-site commissioning records; contact us for site-specific data for your project.